Introduction
Learning how to choose a hex bolt is mostly a matter of reading the order correctly. A hex bolt is not one product: the same M12 bolt can be a soft 4.6 fastener for a fence bracket or a 12.9 alloy bolt for a machine tool, and the two are not interchangeable even though they look identical in a box. The difference is written on the head, in the standard number, and in the coating — and a wrong choice usually shows up only after the joint is loaded, corroded or vibrated loose.
The hex bolt is the most ordered fastener in the world, and the most commonly mis-specified. This guide works through the seven decisions that make up a complete hex bolt specification — standard, property class, thread, material, coating, size and tightening.
1. Start with the standard, not just the size
The standard number controls the bolt’s dimensions. The property class controls its strength. They are two unrelated specifications that happen to travel in the same order line — a DIN 933 bolt can be 4.8 or 12.9 and conform perfectly either way — so always check both. [4]
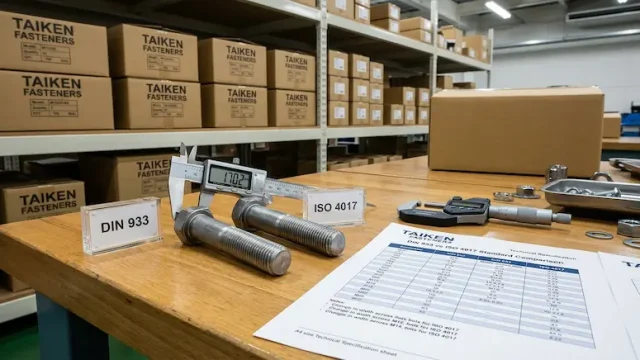
The four metric standards you will meet most often are DIN 931 (partial thread), DIN 933 (full thread), ISO 4014 (partial thread) and ISO 4017 (full thread). [1] The DIN standards were formally withdrawn in favour of their ISO successors, but DIN 931 and DIN 933 are still widely requested, manufactured and used, so the old numbers keep appearing on drawings. [2]
The DIN and ISO bolts are not identical. They share the same thread, but four sizes have a different width across the flats — the distance between two opposite flat sides of the hex head, which decides which wrench fits: [1][2]
| Size | DIN 931 / 933 width across flats | ISO 4014 / 4017 width across flats |
|---|---|---|
| M10 | 17 mm | 16 mm |
| M12 | 19 mm | 18 mm |
| M14 | 22 mm | 21 mm |
| M22 | 32 mm | 34 mm |
At M10, M12 and M14 the ISO head is 1 mm narrower; at M22 the ISO head is 2 mm wider. Every other common size is the same. If the drawing says DIN and the parts arrive to ISO dimensions, a spanner that fits one will not fit the other. [2] The size range differs too: DIN 933 covers M1.6 to M52, while ISO 4017 runs to M64. [2]
For inch-series work and structural connections you will also meet ASTM standards: A307 for low-strength bolts, A449 for high-strength general engineering bolts, and F3125, the standard that replaced the withdrawn A325, for structural steel connections. [1][3] Property classes 8.8, 10.9 and 12.9 map consistently across DIN, ISO and BIS (the Indian system), but they do not map onto ASTM grades, which use a completely separate letter-number system. [3]
2. Read the property class — it is the strength
On a metric carbon-steel bolt the property class is stamped on the head as two numbers separated by a decimal point, for example 8.8. The code is a formula defined by ISO 898-1: the first number times 100 is the nominal tensile strength in MPa, and the second number is the ratio of yield strength to tensile strength. An 8.8 bolt is 800 MPa tensile and yields at about 80% of that, 640 MPa. [5][6]
| Property class | Min. tensile strength | Min. yield strength | Proof stress | Material | Typical use |
|---|---|---|---|---|---|
| 4.6 | 400 MPa | 240 MPa | 225 MPa | Low carbon steel | Light brackets, non-structural work |
| 8.8 | 800 MPa (830 above M16) | 640 MPa (660 above M16) | 580 MPa (600 above M16) | Medium carbon steel, quenched and tempered | General engineering — the workhorse |
| 10.9 | 1,040 MPa | 940 MPa | 830 MPa | Alloy steel, quenched and tempered | Automotive, high-strength joints |
| 12.9 | 1,220 MPa | 1,100 MPa | 970 MPa | Alloy steel, quenched and tempered | Maximum static strength, machinery |
Minimum values per ISO 898-1. [5][6][7]
Three rules keep the choice honest. First, 8.8 is the default for general engineering: it is the first quenched-and-tempered class and the sweet spot between strength and ductility. Second, the step from 8.8 to 10.9 is the biggest strength jump between common grades — about 30% more load capacity. [5] Third, stronger is not always better: 12.9 is the highest standard property class, but also the most brittle, and the wrong choice where the joint sees shock or impact loading. Under dynamic or vibrational loads, the greater ductility of an 8.8 or 10.9 bolt often outlasts a harder 12.9. [5]
Stainless steel bolts use a different marking system under ISO 3506-1, and the two systems must not be mixed up. A stainless designation has two parts: the steel group and the property class, which is the minimum tensile strength divided by ten. A2-70 is a 304-type austenitic stainless bolt with at least 700 MPa tensile strength; A4-80 is a 316-type bolt with at least 800 MPa. [8][9]
| Designation | Steel group | Min. tensile strength | Min. proof stress (Rp0.2) | Typical use |
|---|---|---|---|---|
| A2-70 | A2 (304 type) | 700 MPa | 450 MPa | General-purpose stainless, indoor and light outdoor |
| A4-70 | A4 (316 type, 2–3% molybdenum) | 700 MPa | 450 MPa | Coastal, marine, food and chemical environments |
| A4-80 | A4 (316 type, 2–3% molybdenum) | 800 MPa | 600 MPa | Higher-strength marine and chemical work |
The most common mistake is reading the grade as a strength ranking. A4 is not stronger than A2: an A4-70 and an A2-70 bolt are mechanically identical twins in different alloys. The letter answers the corrosion question; the number answers the strength question. [8][9]
Pair the nut to the bolt (ISO 898-2): class 8 nut with an 8.8 bolt, class 10 with 10.9, class 12 with 12.9. A weaker nut’s thread strips before the bolt reaches full load. [6]
3. Full thread or partial thread
DIN 933 and ISO 4017 bolts are fully threaded; DIN 931 and ISO 4014 bolts are partially threaded, with a plain shank under the head. [1][2]
Choose partial thread when the bolt carries shear load across the joint: the unthreaded shank is stronger in shear than a threaded section of the same diameter. Choose full thread when the joint is mostly in tension, when the plate stack is thin, or when one bolt length should cover several grip lengths. [1]
4. Pick the material for the environment
| Material | Strength range | Corrosion behaviour | Watch out for |
|---|---|---|---|
| Carbon steel, zinc plated | 4.6–12.9 | Thin zinc layer, indoor use | Rusts outdoors within months |
| Carbon steel, hot-dip galvanised | 4.6–10.9 typically | Thick zinc layer, outdoor use | Oversize nuts needed; check thread fit |
| Stainless steel A2 (304) | 500–800 MPa | Good general corrosion resistance | Not for chloride or coastal exposure |
| Stainless steel A4 (316) | 500–800 MPa | Molybdenum resists chlorides and pitting | Costs more; still not for hot chlorides above 60 °C |
Carbon steel is the default where strength per dollar matters and the environment is controlled. Stainless steel is the choice where the bolt will stay wet, or where rust staining would spoil the product — food equipment, architectural work, coastal structures. For chloride exposure, coastal sites and marine equipment, A4 (316) is required; A2 (304) suits most indoor and light-outdoor work. [9][10] Never mix a stainless bolt with a carbon-steel nut, or the reverse, in a wet joint: the two metals form a galvanic couple and the less noble one corrodes faster.
5. Pick the coating for the exposure
A coating is not a colour choice — it is a service-life decision. Zinc protects steel two ways: as a barrier that keeps air and water away, and as a sacrificial layer, because zinc is more reactive than steel, so it corrodes first and protects the exposed steel even where the coating is scratched. The zinc is slowly used up, so a thicker layer simply lasts longer. [11][12]
| Coating | Process | Zinc thickness | Salt-spray life (ASTM B117) | Best for |
|---|---|---|---|---|
| Zinc plated (electroplated) | Electrodeposition in a zinc salt bath | 5–12 µm | 96–120 hours to red rust | Indoor, dry, air-conditioned spaces |
| Hot-dip galvanised (HDG) | Immersion in molten zinc at ~450 °C | 45–85 µm | 1,000+ hours with only minor rust | Outdoor, structural, coastal-adjacent |
| Zinc flake (Dacromet / Geomet) | Zinc and aluminium flakes in a binder | 8–15 µm | Long, with no hydrogen embrittlement risk | High-strength bolts (10.9 / 12.9) outdoors |
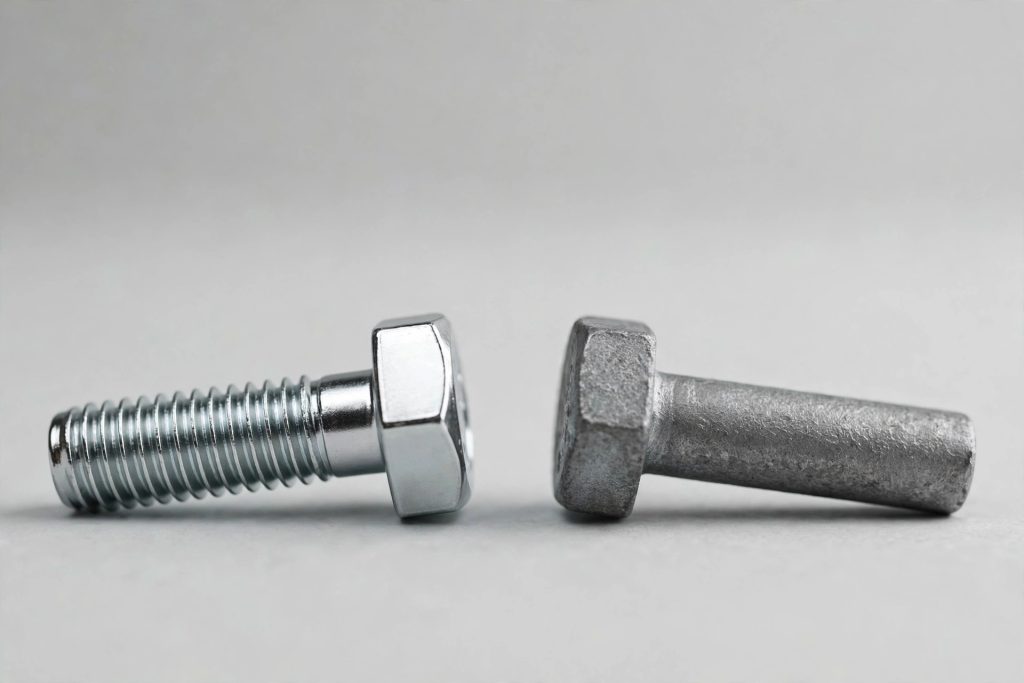
In one side-by-side salt-fog test run for 1,040 hours, the hot-dip galvanised part showed only a few points of rust penetration, while the zinc-plated part was fully covered in thick red rust. [13] Zinc-plated fasteners will typically begin to rust within months of outdoor exposure. [11]
Two practical consequences follow. First, HDG is the standard choice for steel structures, outdoor equipment, fences, scaffolding and bridges exposed to weather. [12] Second, the HDG layer is thick enough that a standard nut will not fit over it — hot-dip galvanised nuts are tapped oversize after galvanising, so always order the nuts with the bolts. [12] For 12.9 bolts, prefer zinc flake over electroplating: plating introduces hydrogen, and a high-strength bolt that has absorbed hydrogen can fail without warning unless it is baked afterwards.
6. Get the size right
Three numbers define a hex bolt: diameter, length and thread pitch. Diameter is the nominal thread diameter — M10 means 10 mm. Length is measured under the head, excluding the head height. Pitch is the distance between threads: coarse is standard (M10 × 1.5, M12 × 1.75); fine (M10 × 1.25, M12 × 1.5) is used where finer adjustment, a thinner wall or better vibration resistance is needed.
Coarse thread is the safer default for site work: it assembles faster, tolerates dirt and minor damage, and is less likely to cross-thread. Fine thread gives a slightly larger tensile stress area and helps in joints that see vibration, but it needs cleaner threads and more careful tapping. If the drawing does not say fine, order coarse.
Measure the grip length — the total thickness of the parts the bolt clamps — and make sure the unthreaded shank, not the thread, sits in the shear plane. Three full threads showing past the nut is a good rule of thumb.
7. Tighten it correctly
A bolt only holds the joint when it is stretched to the right preload, and preload is set by torque. The table below gives torques for dry, unlubricated steel bolts (nut factor K = 0.20, roughly 70% of proof load per ISO 898-1). [14]
| Size | Pitch (mm) | Class 8.8 (N·m) | Class 10.9 (N·m) | Class 12.9 (N·m) |
|---|---|---|---|---|
| M6 | 1.0 | 10 | 14 | 17 |
| M8 | 1.25 | 25 | 35 | 41 |
| M10 | 1.5 | 49 | 69 | 81 |
| M12 | 1.75 | 85 | 120 | 140 |
| M16 | 2.0 | 210 | 295 | 345 |
Two warnings matter more than the numbers. First, lubrication changes everything: an oiled bolt needs roughly 25% less torque for the same clamp force, because the nut factor drops from about 0.20 to 0.15. If you lubricate and use the dry figure, you will over-stress the bolt. [14] Second, torque only controls clamp load when the friction in the joint is known, and installed preload can vary by up to 25% even with a calibrated wrench. For critical joints, confirm the torque against the fastener manufacturer’s data and the joint specification, not against a generic chart. [14]
8. A seven-step buying checklist
Work through these seven steps before the order leaves your desk — each one catches a different class of mistake.
Step 1 — Write the full designation. A complete order line reads like this: “DIN 931 M16 × 80, 8.8, hot-dip galvanised, EN 10204 3.1 certificate.” Standard, size, property class, coating and certificate in one line leaves the supplier nothing to guess.
Step 2 — Check the standard on the drawing. Confirm whether the drawing says DIN or ISO — a 1 mm head difference at M10, M12, M14 or M22 is enough to fail an inspection.
Step 3 — Match the class to the load. Use 8.8 as the default, 10.9 where the joint genuinely needs more clamp force, and 12.9 only for static, high-strength machinery work. Never upgrade a grade to “be safe” without checking ductility and embrittlement.
Step 4 — Match the coating to the exposure. Indoor and dry means zinc plating is fine. Any outdoor, coastal or structural use means HDG or zinc flake. Confirm HDG nuts are tapped oversize.
Step 5 — Check the head marking on arrival. A metric bolt of 5 mm and above must carry the manufacturer’s mark and the property class. A bolt with no readable class has an unknown strength, and no torque chart applies to it. [6][7]
Step 6 — Ask for the certificate — and match it. Ask for the EN 10204 Type 3.1 certificate for your order, with batch-specific test results tied to a heat number, and check that the heat number matches the packaging and the parts. A 2.1 declaration only states compliance and gives no test results.
Step 7 — Test a sample. For first orders or large shipments, check hardness and dimensions on a sample from the actual lot. A portable Rockwell tester catches an unhardened bolt in seconds: 8.8 should read HRC 22–32, 10.9 HRC 32–39, 12.9 HRC 39–44. [6]
9. Frequently asked questions
Q1: Is a stainless A4-70 bolt stronger than an A2-70 bolt?
No. Both meet the same 700 MPa minimum tensile strength; the difference is entirely in corrosion performance, because A4 (316) contains molybdenum and A2 (304) does not. The letter is the alloy; the number is the strength. [8][9]
Q2: Can I use a 10.9 bolt where the drawing says 8.8?
Mechanically it is stronger, but do not substitute without checking. A 10.9 bolt is less ductile, needs a higher tightening torque and a class 10 nut, and it changes the failure mode of the joint. Ask the design authority first.
Q3: Why won’t my nut fit on a hot-dip galvanised bolt?
The HDG zinc layer is 45–85 µm thick, enough to stop a standard nut from fitting. Hot-dip galvanised nuts are tapped oversize after galvanising so they fit. Always order the nuts with the bolts. [12]
Q4: How do I read the numbers on a metric bolt head?
The first number times 100 is the nominal tensile strength in MPa; the second number is the yield ratio. An 8.8 bolt is 800 MPa tensile with a yield of about 640 MPa; a 10.9 bolt is 1,040 MPa tensile with a yield of about 940 MPa. [5][6]
10. A short note on how Taiken works
Taiken is based in Yongnian, Handan — China’s largest fastener cluster — and consolidates bolts, nuts, screws, washers and custom parts from qualified factories in the area into one order, one quality standard and one shipment. [15] Hex bolts are supplied in property classes 4.6 to 12.9 and in A2-70 and A4-80 stainless, to DIN 931/933 and ISO 4014/4017, with zinc plating, hot-dip galvanising and zinc flake finishes. Material heat numbers are tracked and samples kept per batch; orders go through dimensional, hardness, tensile and coating checks, with certificates tied to the factory that made the goods, and third-party testing can be arranged on request. [15]
If you need hex bolts, send your standard list, bill of materials or drawing, with the standard, size, property class, coating and quantity for each item. Taiken confirms missing details before quoting and usually replies within 24–48 hours. [15]
Sources
- How to Choose Hex Bolts: Standard, Property Class, Finish and Supplier — DIN 931/933 vs ISO 4014/4017, partial vs full thread, WAF differences (Global Fasteners Exports): https://www.globalfastenersexports.com/guides/how-to-choose-hex-bolts
- DIN 933 vs DIN 931: ISO 4017, ISO 4014, IS 1364 — withdrawn DIN standards, WAF at M10/M12/M14/M22, size ranges (Induskart): https://www.induskart.co.in/din-933-vs-din-931-hex-bolts/
- DIN vs ISO vs ASTM: Understanding Fastener Standards — the five systems, property-class mapping, structural bolt equivalents (Global Fasteners Exports): https://www.globalfastenersexports.com/blog/din-vs-iso-vs-astm-fastener-standards
- DIN 931, 933 and 934: Why the Standard Number Is the Order — standard controls dimensions, class controls strength (DC Screws): https://www.dcscrews.com/info/din-931-933-934-hex-bolt-nut-standard-guide-103737080.html
- Bolt Grade Strength Chart: 8.8 vs 10.9 vs 12.9 Guide — ISO 898-1 property-class values, hardness, 30% jump from 8.8 to 10.9 (Prince Fastener): https://princefastener.com/bolt-grade-strength-chart-8-8-vs-10-9-vs-12-9-guide/
- Bolt grades explained: 4.6 to 12.9, strength, hardness and the steel behind each — full ISO 898-1 table, hardness ranges, nut pairing (KB Fasteners): https://kbfasteners.in/blog/bolt-grades-explained
- Metric Bolt Torque Chart: M3 to M39, Class 8.8, 10.9, 12.9 — ISO 898-1 proof/tensile/yield values by class (MLC): https://mlc.org.uk/guides/metric-bolt-torque-chart
- A2 and A4 Stainless Steel: ISO 3506 Property Classes — A2 is 304 type, A4 is 316 type, class is tensile/10, ISO 3506-1:2020 (Laxcon Steels): https://www.laxconsteels.com/a2-a4-stainless-steel-iso-3506/
- Stainless Steel Fasteners: A2, A4, 70 & 80 Explained — A4-70 vs A2-70 same strength, different corrosion; Rp0.2 values (Vision Alloys): https://www.visionalloys.com/blog/stainless-steel-fasteners-a2-a4-70-80-explained/
- Stainless Fastener Grades: A2 vs A4, -70 vs -80 (304 vs 316) — A2 for indoor/light outdoor, A4 for chloride and marine (AIMS Industrial): https://aimsindustrial.com.au/blogs/product-guides/stainless-steel-fasteners-guide
- Zinc Plated vs Galvanised vs Stainless: Bolt Coatings — coating thickness, salt-spray hours, zinc-plated rusts outdoors within months (AIMS Industrial): https://aimsindustrial.com.au/blogs/product-guides/zinc-plated-vs-galvanised
- HDG vs GI vs Zinc-Plated Fasteners — ISO 10684 coating thickness, oversize tapped HDG nuts, UAE outdoor guidance (Mufaddal Fasteners): https://www.mufaddalfasteners.com/blog/hdg-vs-gi-vs-zinc-plated-fasteners
- HDG vs Zinc Plate Comparison — 1,040-hour salt-fog test, HDG vs plated, ASTM A153 vs B633 (Hubbell / CHANCE): https://hubbellcdn.com/testdoc/HDGvsZinc-Plate-Comparison.pdf
- Metric Bolt Torque Chart: M3 to M39, Class 8.8, 10.9, 12.9 — dry-thread torques, K = 0.20, ~70% of proof load, lubrication reduces torque ~25% (MLC): https://mlc.org.uk/guides/metric-bolt-torque-chart
- Taiken Fasteners — homepage: https://taikenfasteners.com/